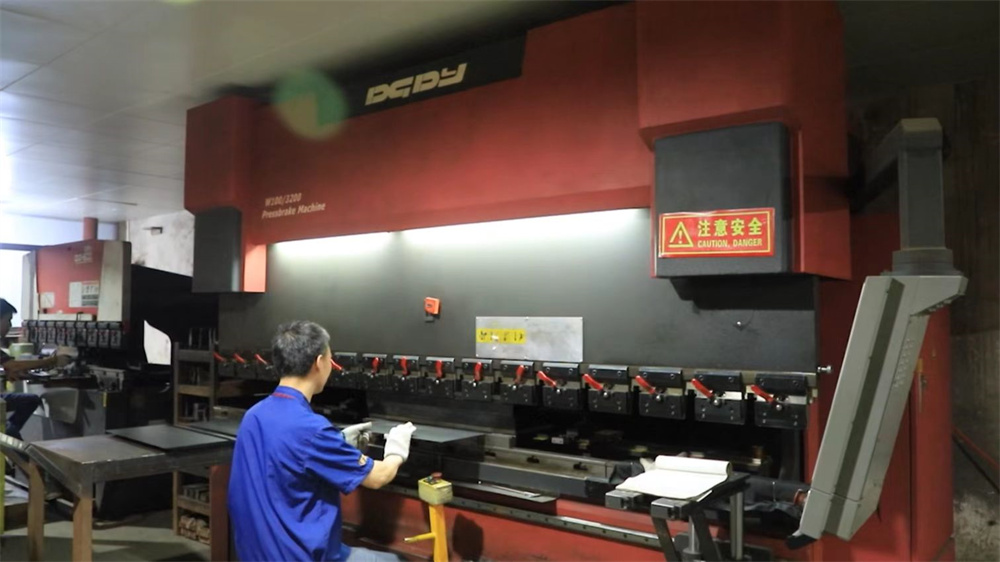
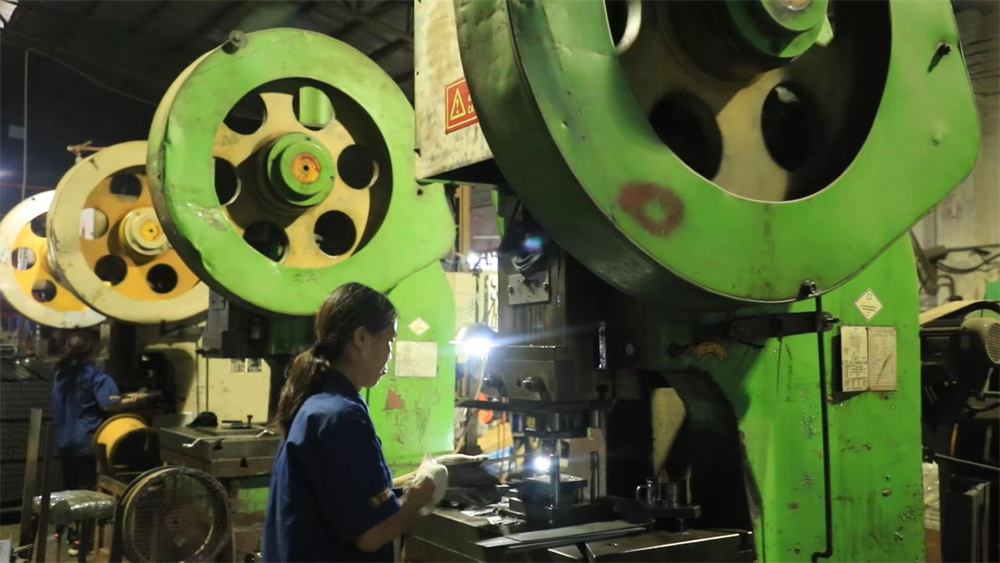
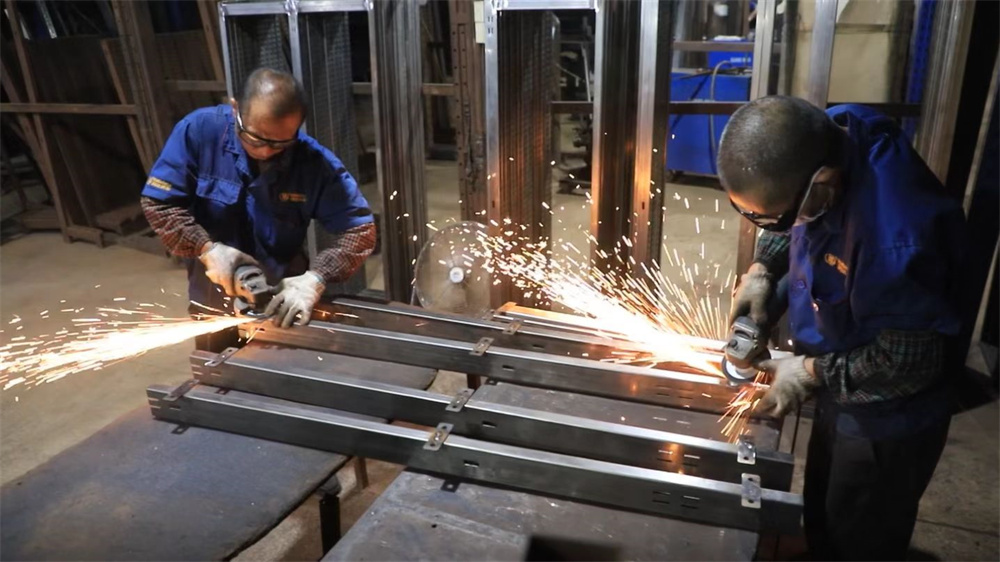
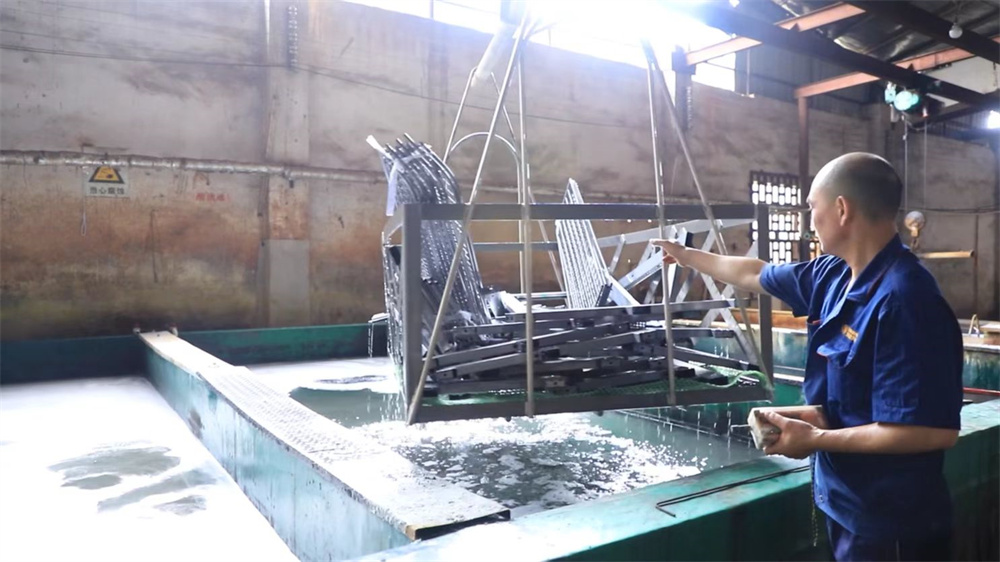
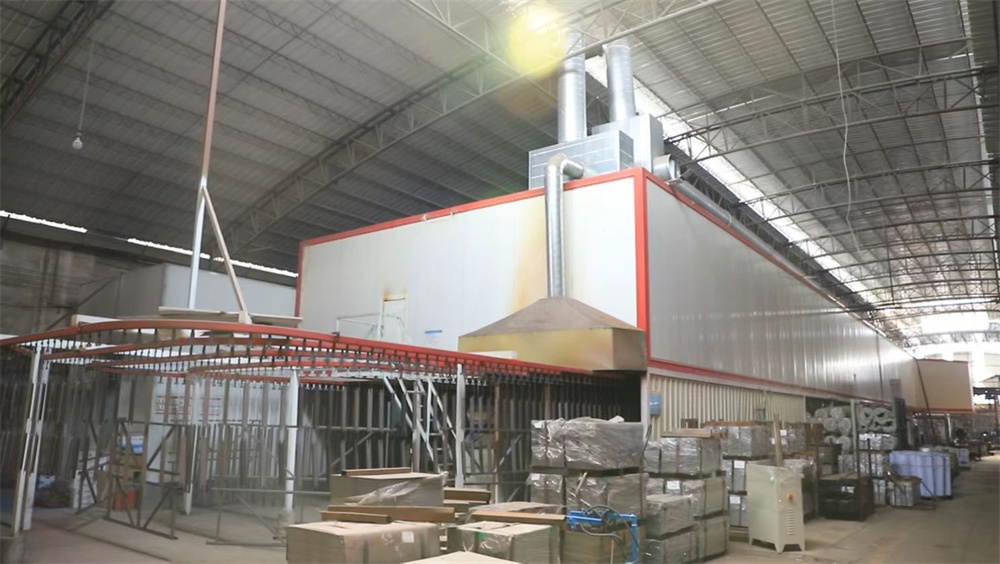
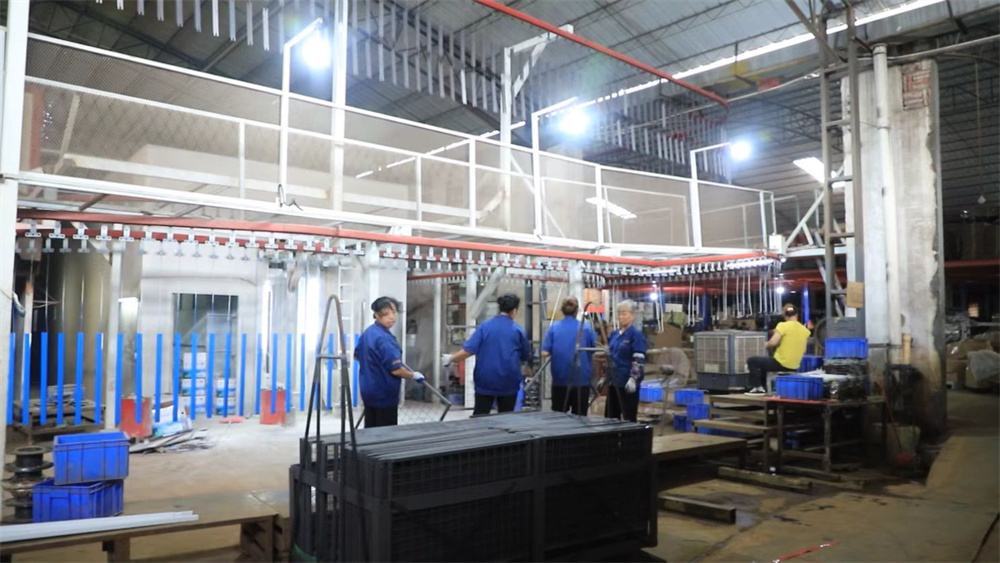
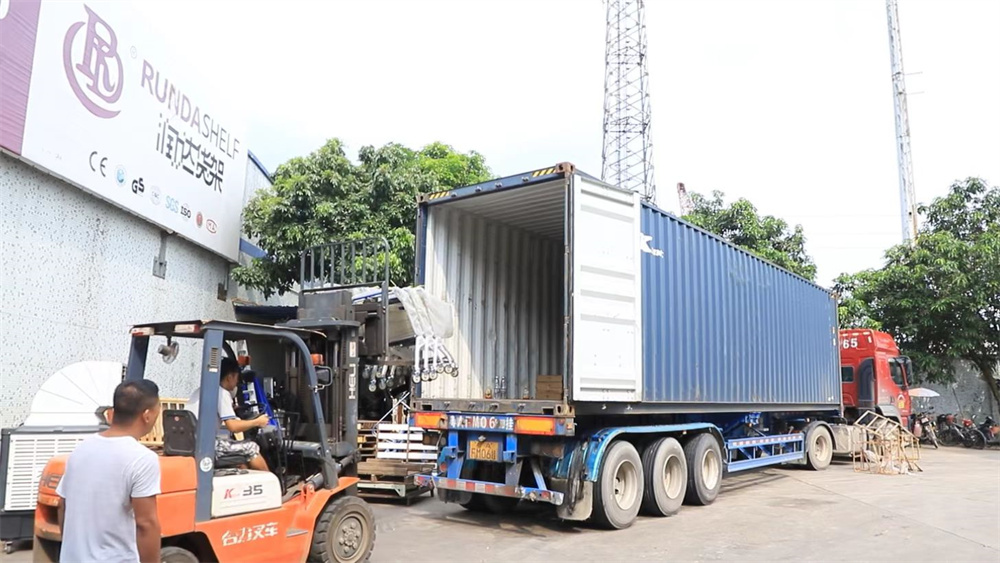
Established in 2017, Chengdu DriveRacks Industrial Technology Co., Ltd. operates a state-of-the-art 42,000 m² manufacturing plant dedicated to advanced material handling and heavy-duty storage infrastructure. Delivering $35 million in annual export revenue, we bring 9 years of deep industry expertise and 6 years of international trade operations. Quality is integral to our process; our team of 30 certified inspectors executes rigorous raw material tensile testing and automated powder-coating thickness audits. Serving high-growth markets across the Middle East, Latin America, and Oceania, DriveRacks leverages a robust ecosystem of 1,200 supply chain partners. We primarily serve enterprise warehouse operators, e-commerce fulfillment hubs, and heavy equipment manufacturers. Powered by 110 skilled R&D engineers focusing on smart automation and high-density racking design, we released 250 dynamic product iterations last year and provide comprehensive customization spanning rack dimensions, seismic ratings, and surface treatments.
The global retail and warehousing ecosystem is undergoing a profound structural transformation driven by the exponential growth of e-commerce, omni-channel retail fulfillment, and hyper-dense supply chain demands. Modern distribution centers and mega-retailers require integrated merchandising solutions that transcend traditional passive storage. Today's industrial environment demands smart inventory management, seamless material handling flow, and high-impact retail visual merchandising fixtures that maximize space utilization while minimizing operational bottlenecks.
As international supply chains face persistent cost pressures and labor shortages, procurement directors across North America, Europe, the Middle East, Latin America, and Oceania are actively seeking Tier-1 Chinese manufacturing partners. These enterprises require suppliers who can deliver engineered reliability, compliance with international seismic and structural standards, and agile custom manufacturing capabilities at scale.
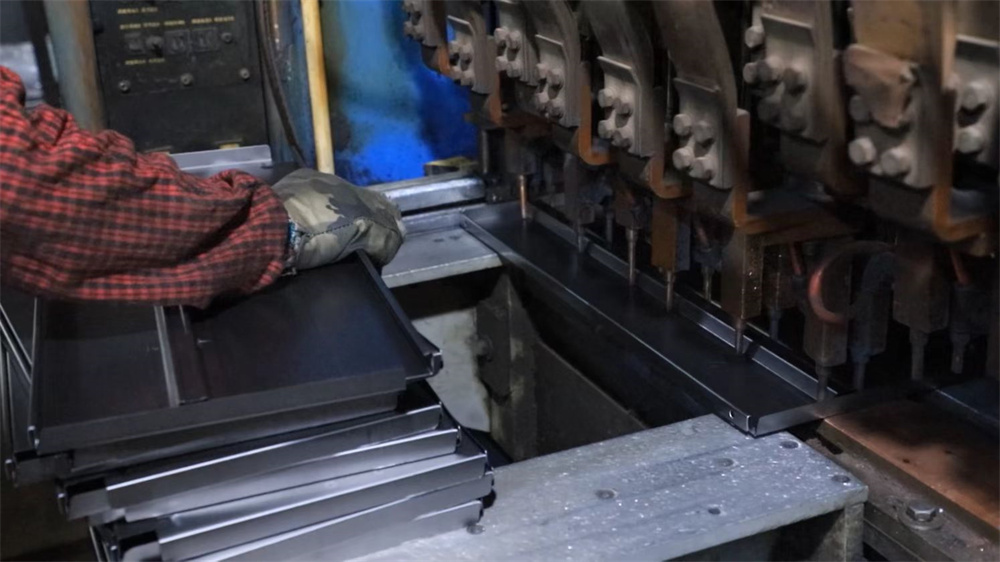
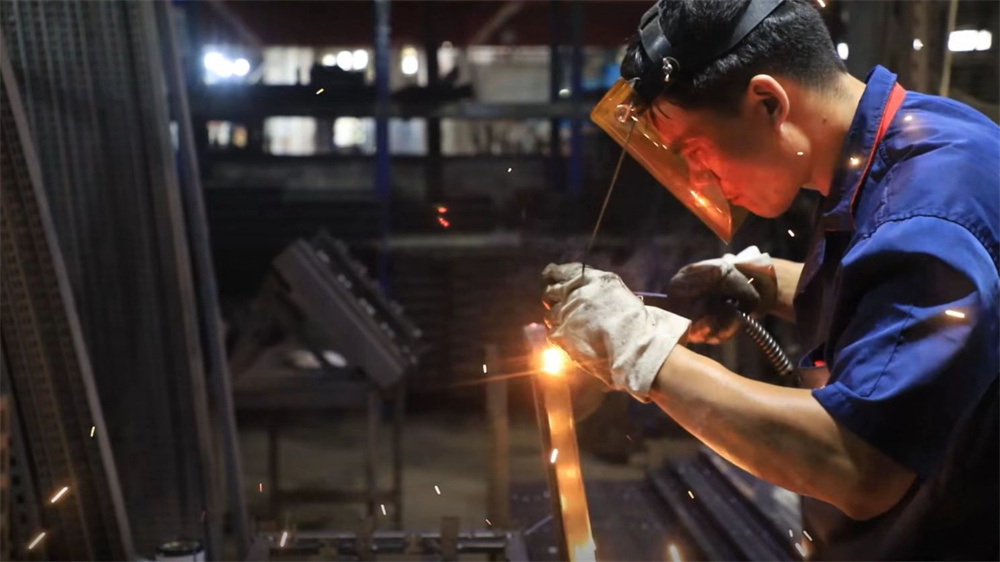
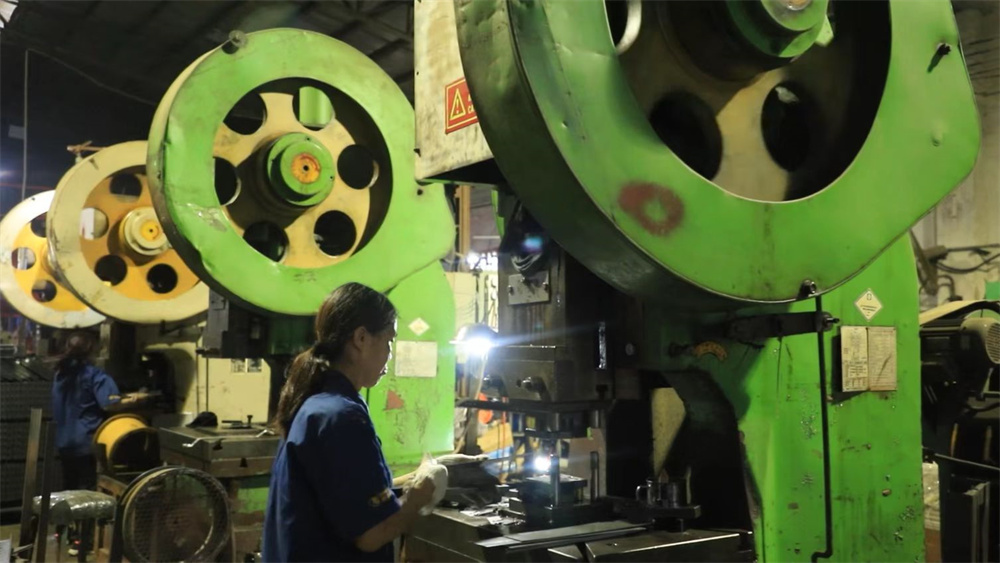
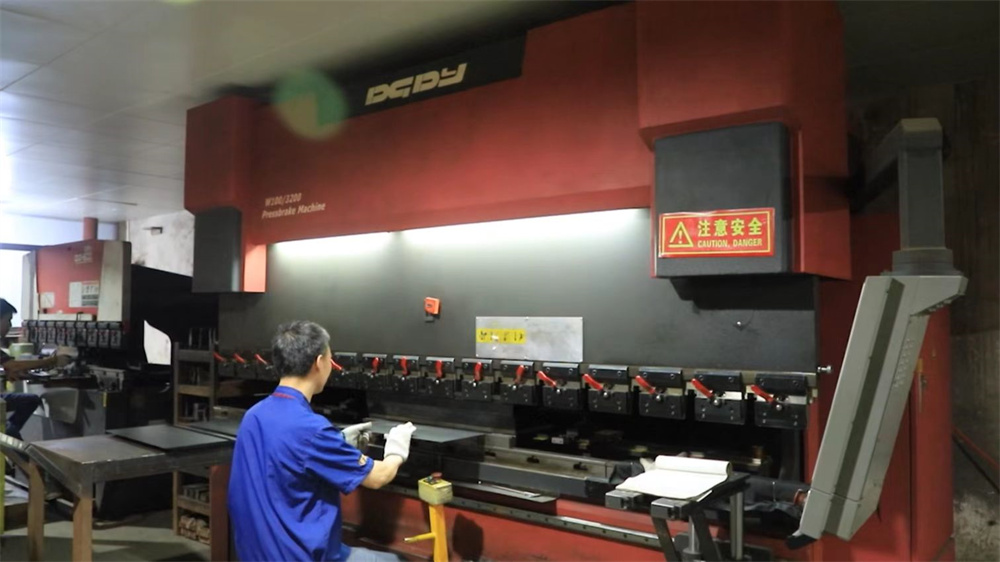
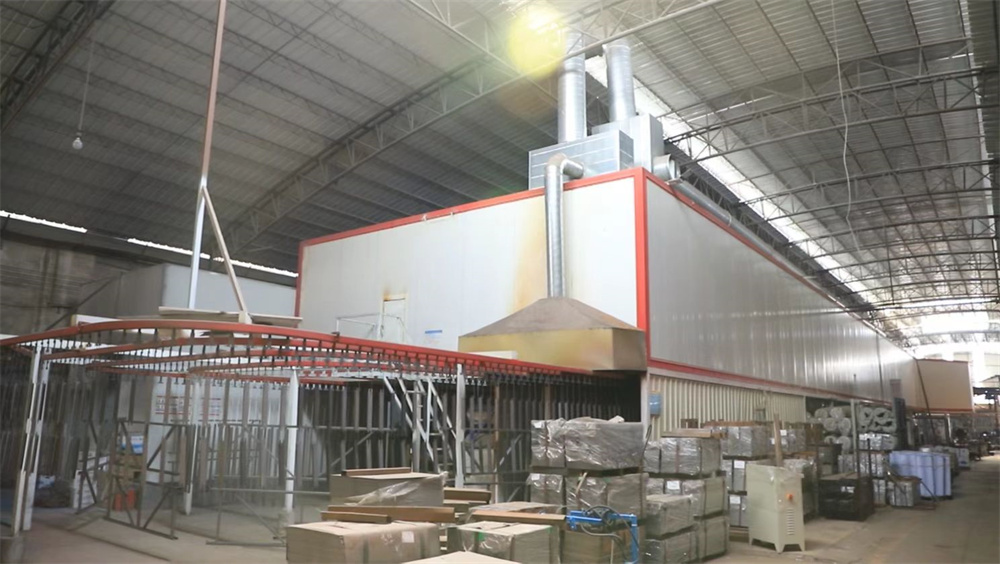
China has established an unassailable leadership position as the global hub for heavy-duty storage and commercial merchandising solutions. This dominance is anchored in a comprehensive industrial cluster effect, advanced metallurgy R&D, and heavily automated manufacturing execution systems (MES). Chinese manufacturing facilities integrate computerized numerical control (CNC) laser cutting, robotic welding arms, and automated electrostatic powder coating lines to achieve tolerances measured in fractions of a millimeter.
Furthermore, the integration of 1,200+ specialized tier-2 component suppliers within close geographic proximity enables unprecedented supply chain velocity. This structural efficiency allows export-oriented suppliers like DriveRacks to compress lead times, optimize raw material input costs, and deliver superior ROI to global enterprise buyers without ever compromising on material grade or structural integrity.
Effective merchandising and warehouse solutions are not one-size-fits-all; they must be meticulously tailored to specific operational environments and localized regulatory frameworks:
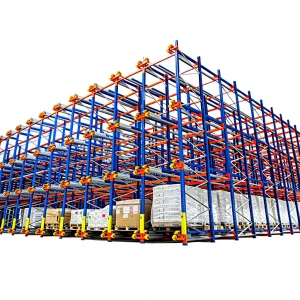
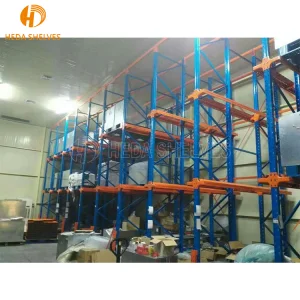
1. Automated Cold Storage Logistics: In temperature-controlled distribution centers, materials must withstand sub-zero conditions without structural embrittlement. High-density radio shuttle racks and galvanized steel structures prevent corrosion and maximize cubic capacity where energy costs per square meter are exceptionally high.
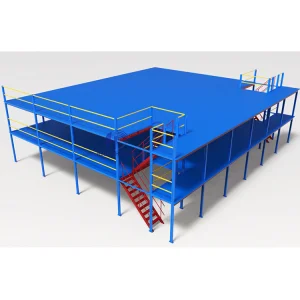
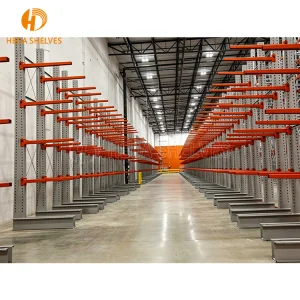
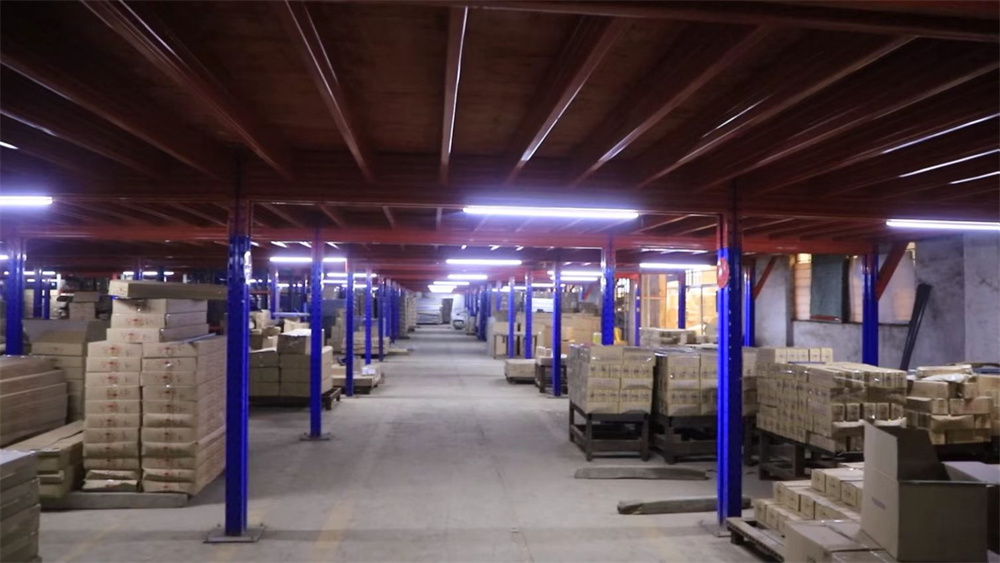
2. Multi-Tier E-Commerce Fulfillment Hubs: Rapid order picking requires robust industrial mezzanine flooring systems and cantilever racking that support high foot traffic, automated guided vehicles (AGVs), and heavy pick-face inventories.
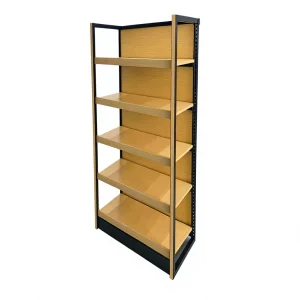
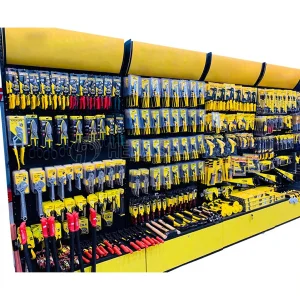
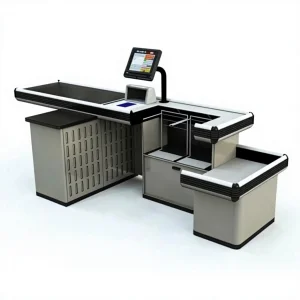
3. Commercial Retail & Big-Box Supermarkets: Aesthetic durability meets functional merchandising through modular gondola shelving, check-out counters, and specialized tool display racks designed to optimize consumer dwell time and inventory turnover.
 DriveRacks