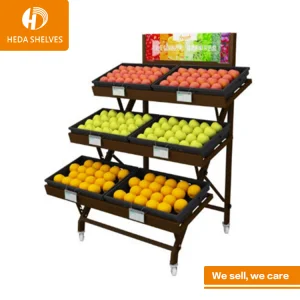
High-precision commercial merchandising equipment engineered for maximum retail efficiency and modular adaptability.
Setting global benchmarks in manufacturing scalability, quality control, and intelligent storage infrastructure.
Established in 2017, Chengdu DriveRacks Industrial Technology Co., Ltd. operates a state-of-the-art 42,000 m² manufacturing plant dedicated to advanced material handling and heavy-duty storage infrastructure. Delivering $35 million in annual export revenue, we bring 9 years of deep industry expertise and 6 years of international trade operations. Quality is integral to our process; our team of 30 certified inspectors executes rigorous raw material tensile testing and automated powder-coating thickness audits. Serving high-growth markets across the Middle East, Latin America, and Oceania, DriveRacks leverages a robust ecosystem of 1,200 supply chain partners. We primarily serve enterprise warehouse operators, e-commerce fulfillment hubs, and heavy equipment manufacturers. Powered by 110 skilled R&D engineers focusing on smart automation and high-density racking design, we released 250 dynamic product iterations last year and provide comprehensive customization spanning rack dimensions, seismic ratings, and surface treatments.
Analyzing macroeconomic shifts, retail evolution, and supply chain resilience in the post-pandemic industrial era.
Modern retail environments demand agility. Omni-channel integration requires product displays and warehouse storage systems that transition smoothly from back-end high-density pallet racking to customer-facing merchandising gondolas.
Global disruption highlights the necessity of robust manufacturing ecosystems. China's industrial clusters offer unmatched component integration, automated fabrication, and economies of scale that stabilize international procurement.
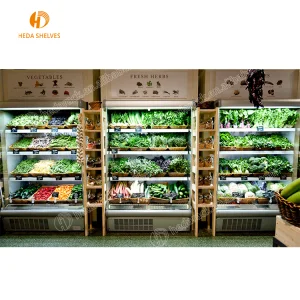
Labor shortages and rising operational expenditures accelerate the adoption of automated storage and retrieval systems (ASRS), radio shuttle racks, and smart temperature-controlled retail display fixtures.
Pioneering the next generation of smart material handling and IoT-enabled modular display configurations.
Embedding weight sensors and RFID tracking directly into display shelving and heavy-duty pallet racks for real-time inventory visibility and automated replenishment alerts.
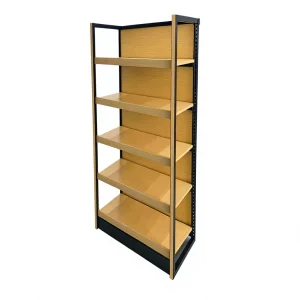
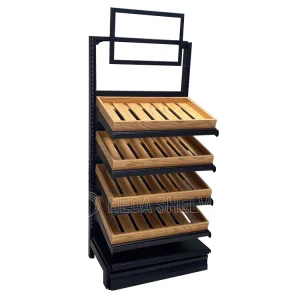
Transitioning toward carbon-neutral steel processing, solvent-free powder coating formulations, and recyclable modular timber-metal hybrid display structures.
Deploying generative AI design tools that allow enterprise clients to configure bespoke warehouse layouts and retail display floors with instant structural load simulations.
Meeting rigorous international engineering codes across diverse regulatory environments worldwide.
Different global regions present unique operational challenges. In earthquake-prone zones across Latin America and parts of Oceania, our structural engineers integrate reinforced seismic bracing and specialized base plate anchors. For humid Middle Eastern and coastal retail sectors, multi-stage anti-corrosion treatments and galvanized steel configurations guarantee structural longevity.
Compliance is non-negotiable in industrial infrastructure. Our manufacturing workflows strictly adhere to ISO9001 quality management standards, CE safety directives, and FEM (European Racking Federation) guidelines. Each product batch undergoes rigorous tensile strength testing, load-bearing verification, and salt-spray corrosion evaluations before international dispatch.
A transparent look into our 42,000 m² high-tech production line, from raw material inspection to automated final dispatch.
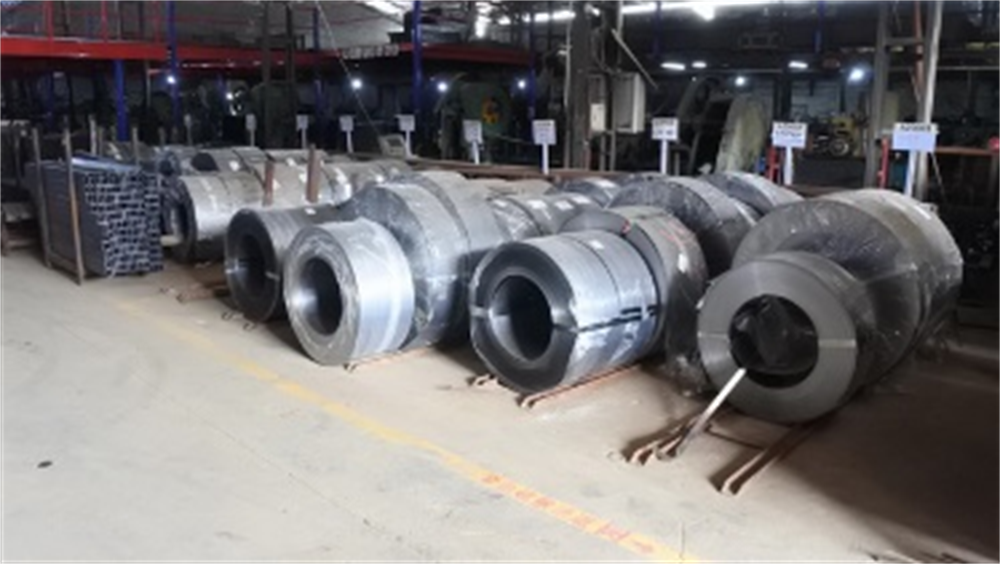
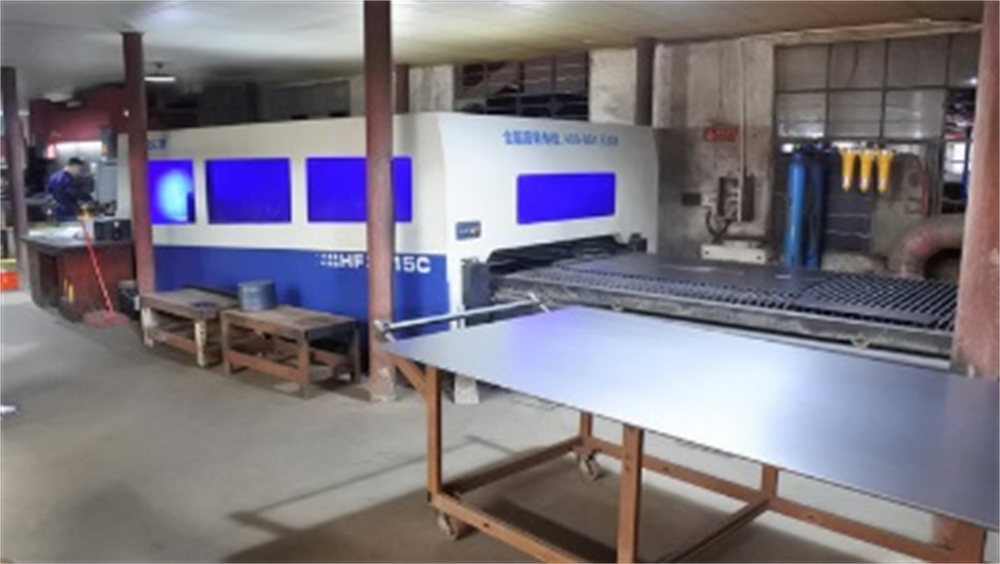
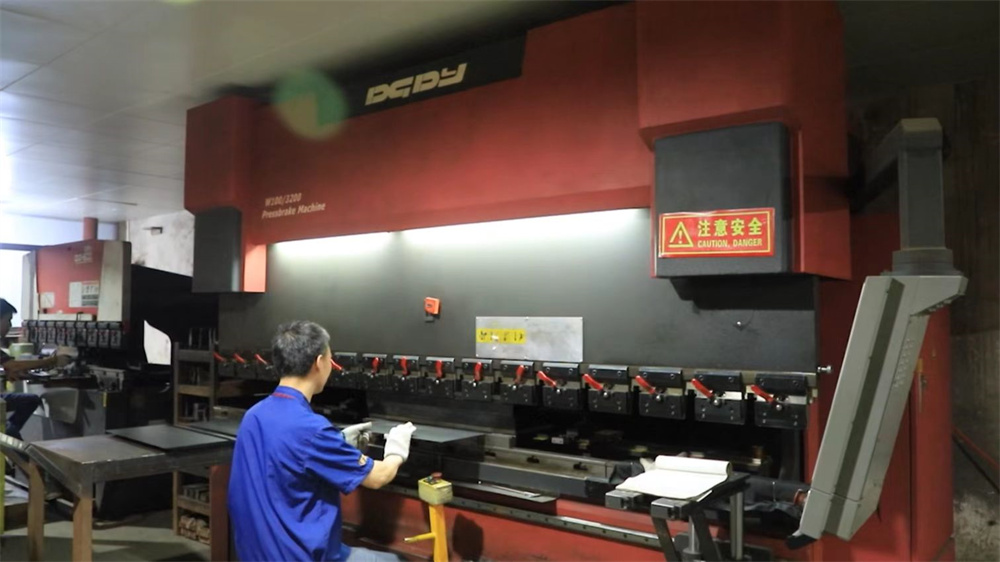
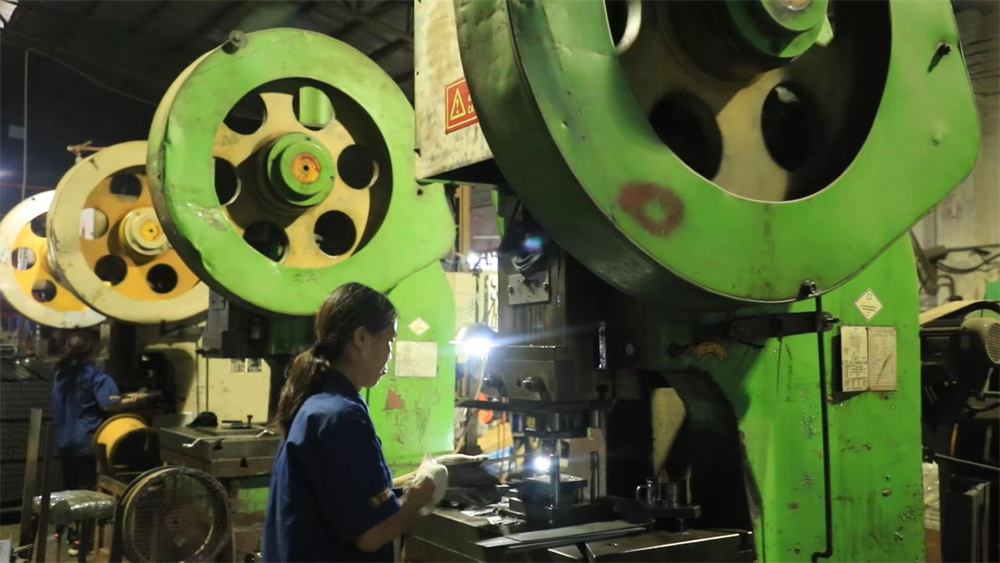
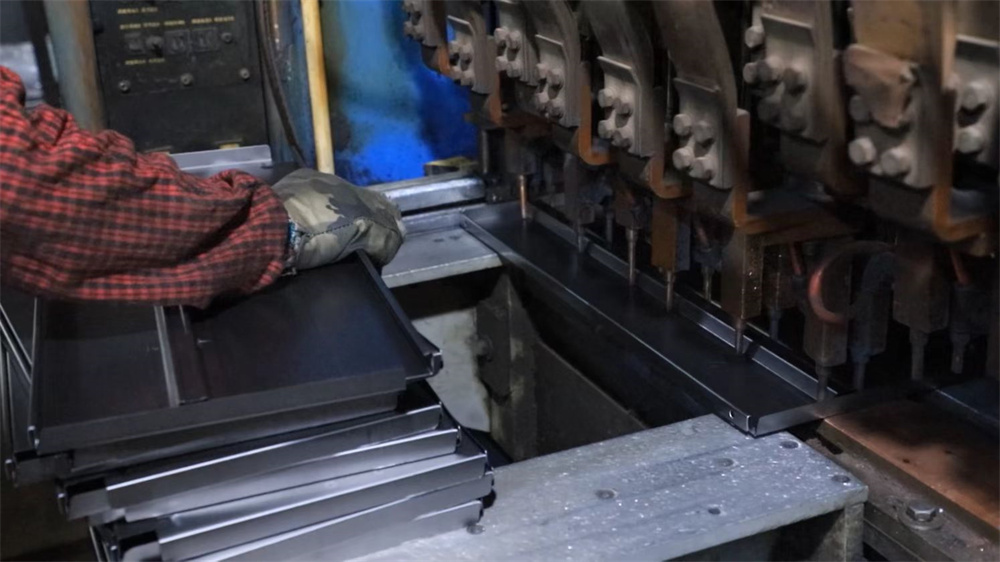
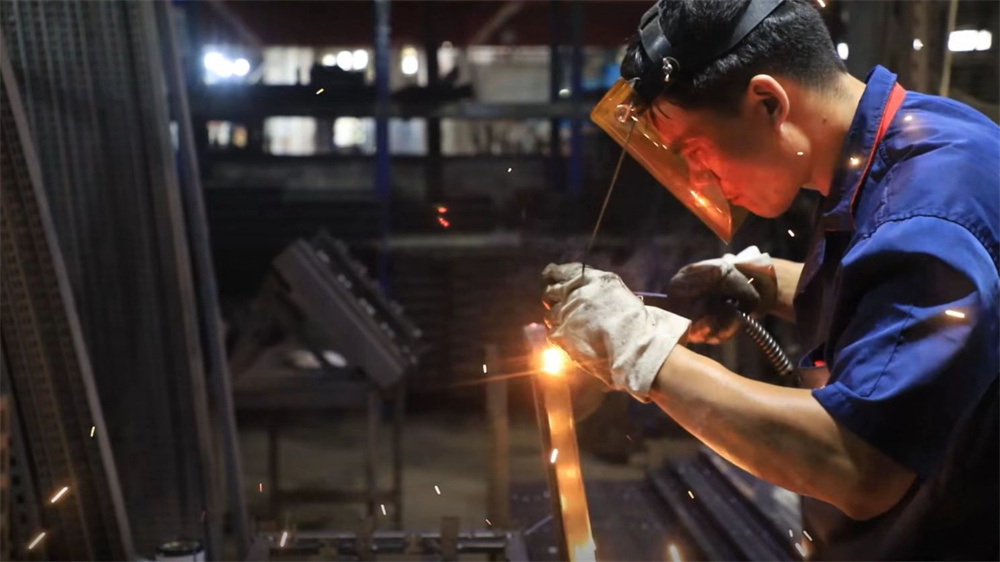
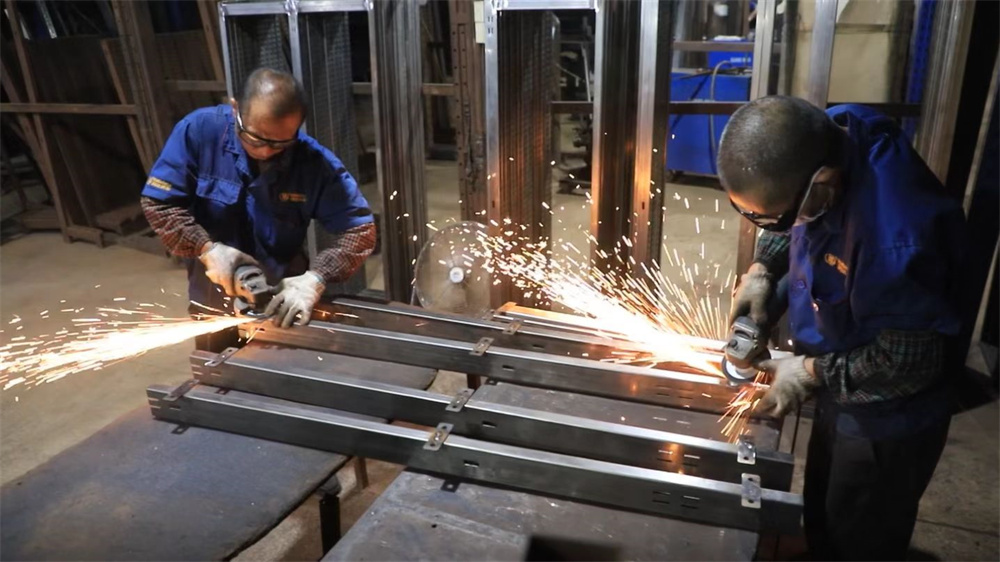
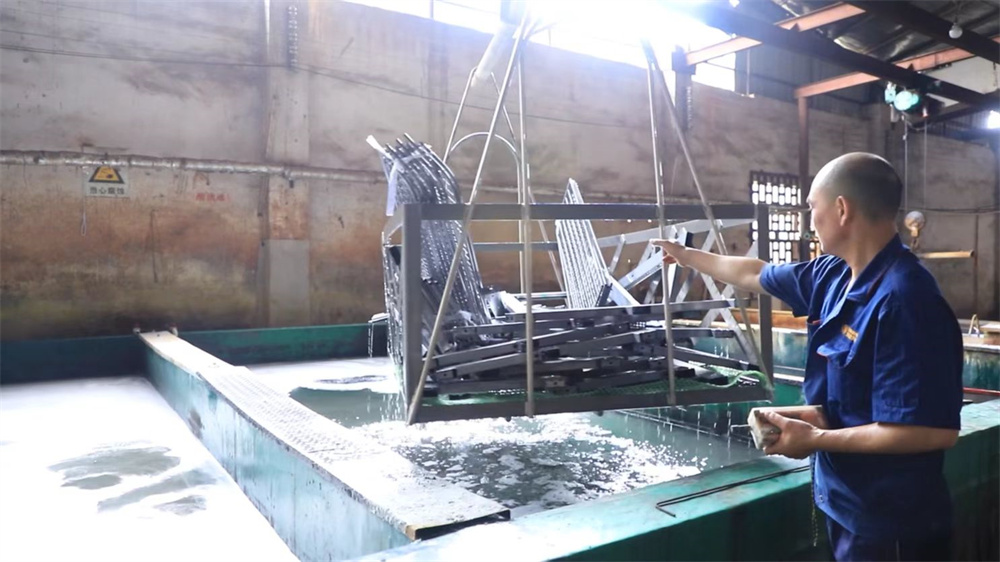
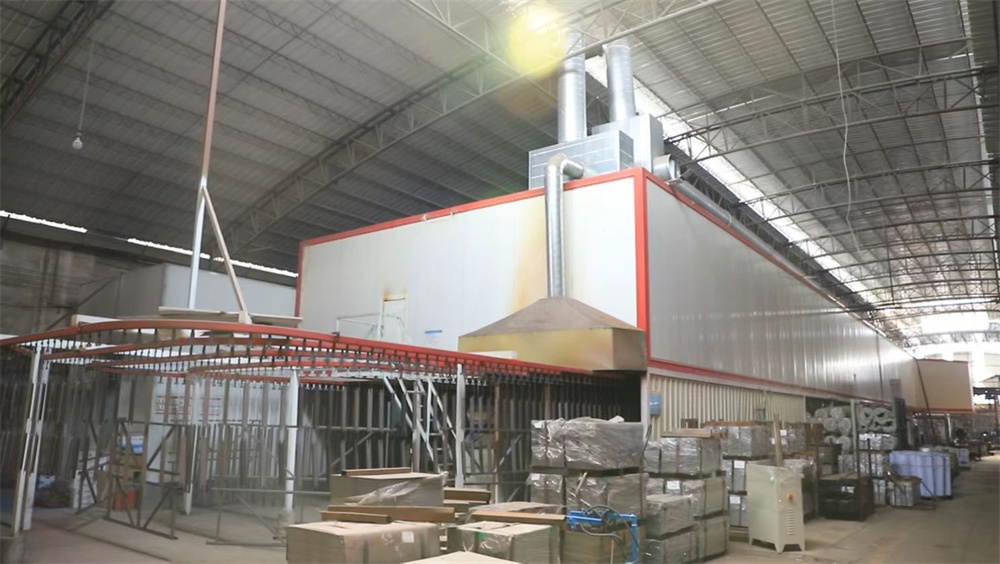
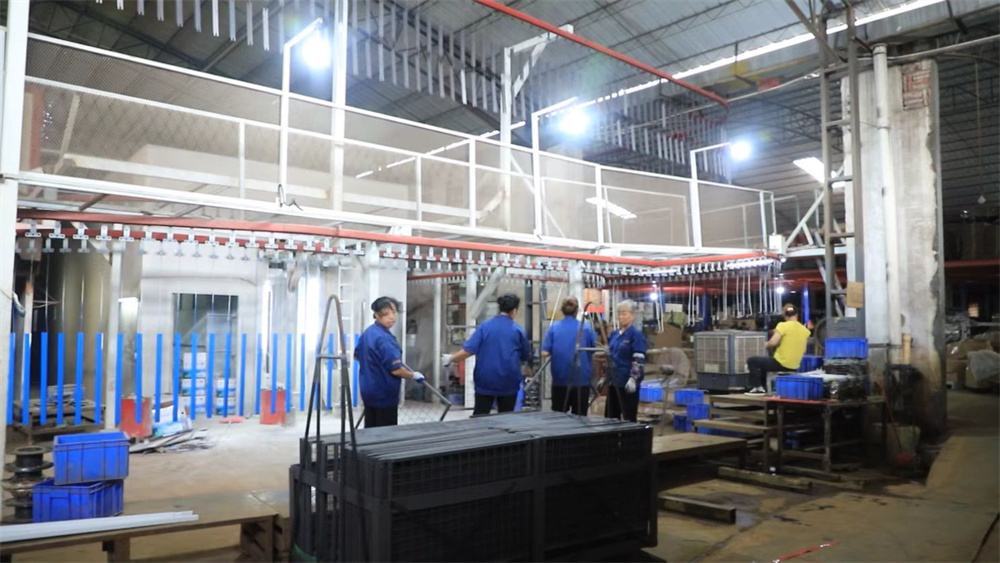
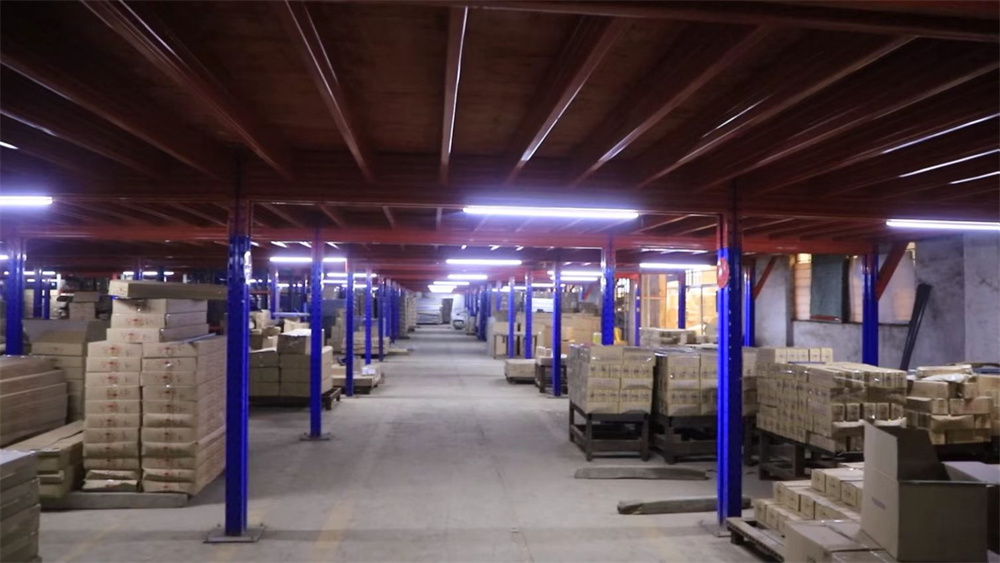
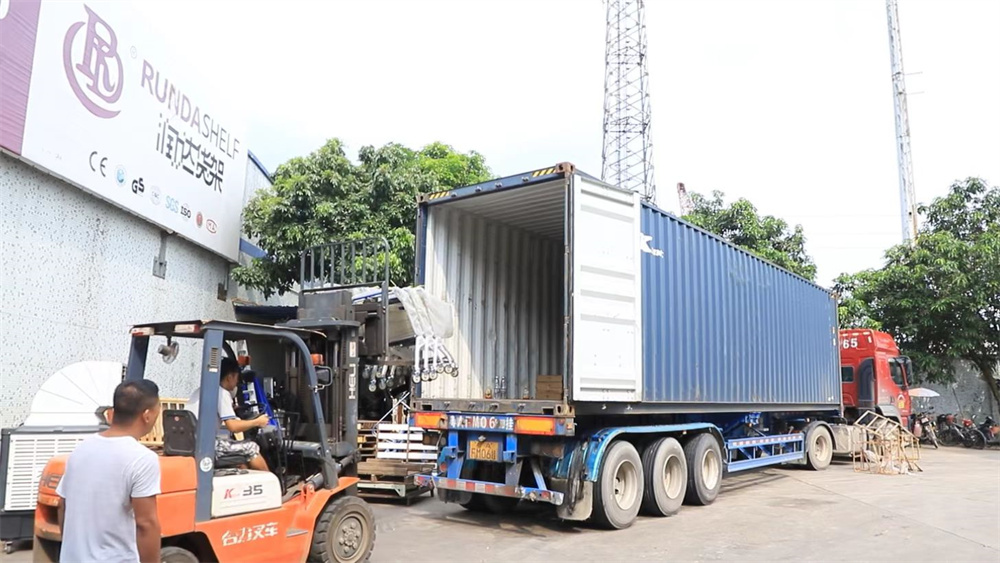
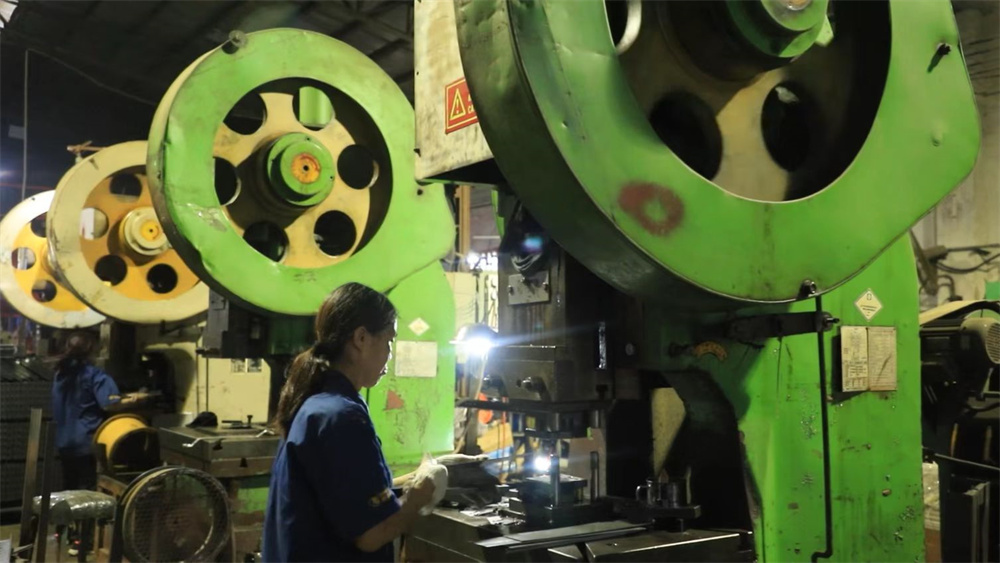
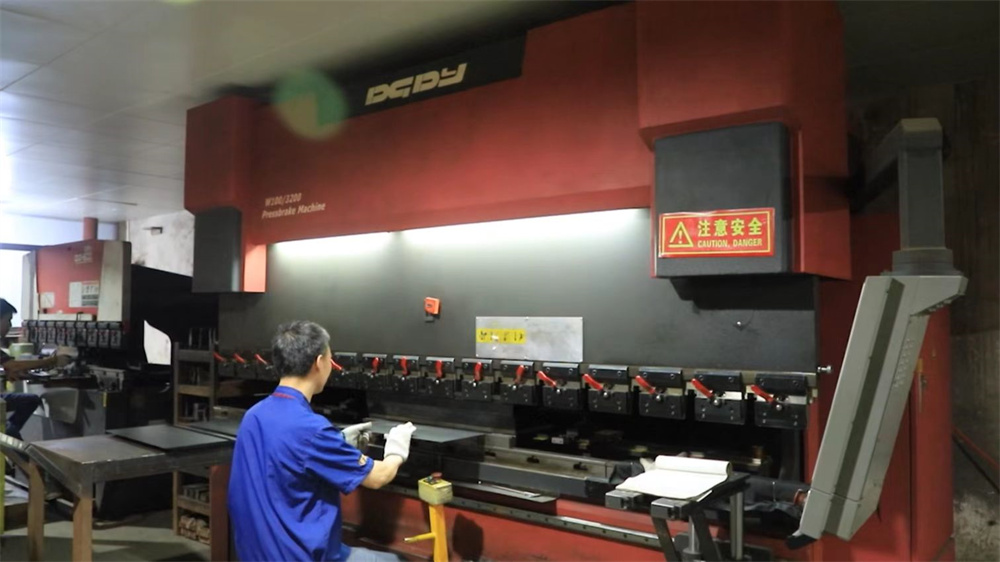
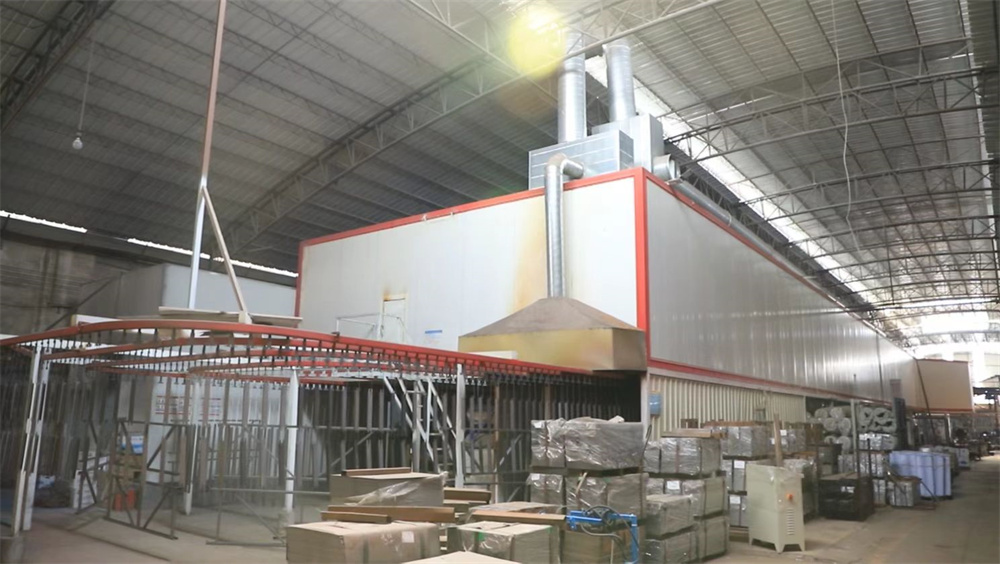
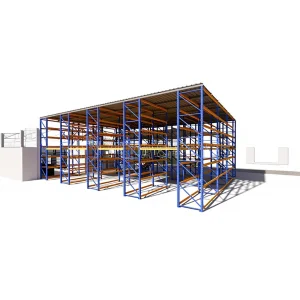
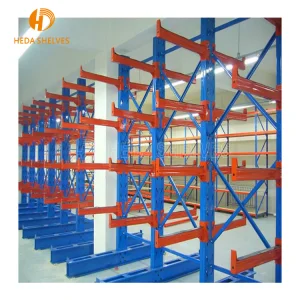
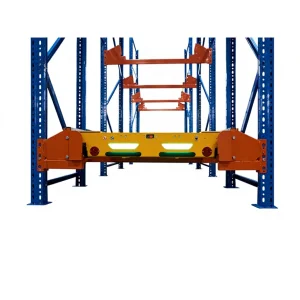
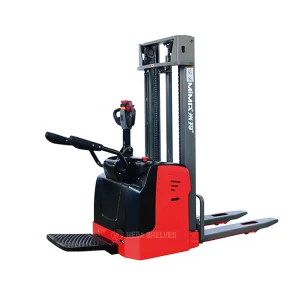
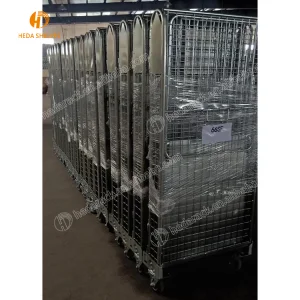
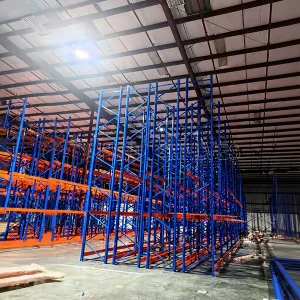
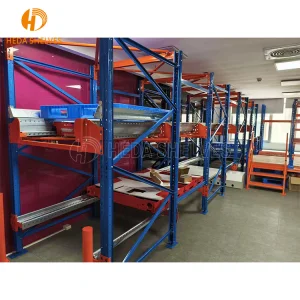
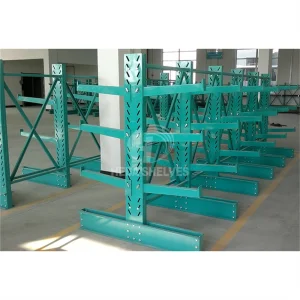
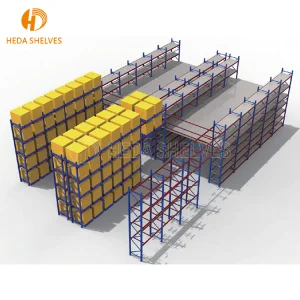
Heavy-duty warehouse racking systems, automated shuttles, and specialized transport units built for ultimate durability.
Expert answers regarding OEM/ODM customization, lead times, and global shipping standards.
We provide comprehensive customization including specific dimensions, load-bearing capacities, seismic ratings, bespoke powder-coating colors, and hybrid material combinations (such as steel and wood grain finishes).
Thanks to our 42,000 m² automated manufacturing plant and robust 1,200+ supply chain network, standard production cycles range between 15 to 25 days depending on project scale and custom engineering specifications.
Our 30 certified inspectors execute rigorous raw material tensile tests and automated powder-coating thickness audits. All structural components undergo premium anti-corrosion treatments and protective export packaging.
We actively supply high-growth enterprise warehouse operators, e-commerce fulfillment hubs, and major retail chains across the Middle East, Latin America, Oceania, and global markets.
 DriveRacks